Fast turnaround times Industrial Chemicals manufacturer from China
Zhengzhou Mahaco Industrial Co., Ltd. (M.H.C) is a professional supplier and manufacturer of high-quality industrial chemicals based in Zhengzhou, China. Known for fast turnaround times, the company offers a comprehensive portfolio including water treatment chemicals (PAC, PFS, PolyDADMAC, etc.), detergent raw materials (SLES, STPP, etc.), industrial acids and alkalis (Nitric Acid 68%, Caustic Soda, etc.), and specialty additives (Zinc Sulphate, Hexamine). Leveraging its strategic location in Central China’s transportation hub, M.H.C ensures rapid delivery to major ports and international clients. The company maintains strict quality control through partnerships with ISO-certified manufacturers and provides certificates of analysis for every batch. Its one-stop sourcing model reduces procurement complexity, while flexible packaging (bags, drums, IBC totes, flexitanks) and professional documentation support facilitate seamless global trade. With a proven track record across Asia, Africa, South America, and Europe, M.H.C is a trusted partner for industries such as water treatment, cosmetics, mining, and food processing, delivering reliability and speed in every shipment.
In the dynamic world of industrial chemicals, speed and reliability are paramount. Zhengzhou Mahaco Industrial Co., Ltd. (M.H.C), based in the strategic transportation hub of Zhengzhou, Central China, has emerged as a leading supplier and manufacturer known for its fast turnaround times and comprehensive product portfolio. This article explores how M.H.C’s one-stop sourcing, rigorous quality control, and logistics advantages make it the preferred partner for global buyers seeking high-quality industrial chemicals.
About Zhengzhou Mahaco Industrial Co., Ltd.
Zhengzhou Mahaco Industrial Co., Ltd. (abbreviated as Mahaco or M.H.C) is a professional supplier and manufacturer of high-quality industrial chemicals, serving clients worldwide. With years of experience in the chemical trading industry, M.H.C has built a professional team dedicated to quality control, logistics management, and customer service. The company’s business philosophy centers on integrity, reliability, and mutually beneficial partnerships. By maintaining strong relationships with reputable manufacturers and implementing strict quality inspection processes, M.H.C ensures that every shipment meets customer specifications and international standards.
Core Business and Product Portfolio
M.H.C specializes in the sourcing, distribution, and supply of a comprehensive range of chemical products. Their offerings include water treatment chemicals, detergent raw materials, industrial inorganic acids and alkalis, and various chemical auxiliaries. Serving industries such as water treatment, cosmetics and detergents, mining, food processing, and general industrial manufacturing, the company provides tailored solutions for diverse applications.
Water Treatment Chemicals (Complete Range)
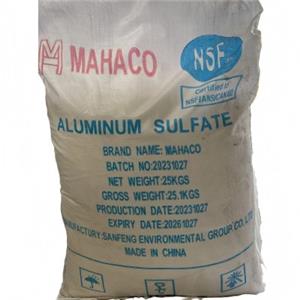
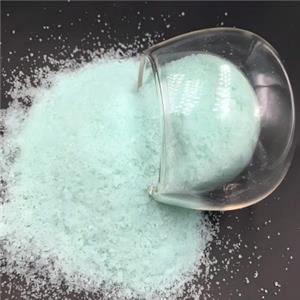
M.H.C supplies a full line of water treatment solutions for both potable water and wastewater applications. Key products include Poly Aluminium Chloride (PAC) available in regular and white powder grades, Poly Ferric Sulphate (PFS), PolyDADMAC as a coagulant, Aluminium Sulphate Ironless 17%, Sodium Hexametaphosphate (SHMP 68%), and Activated Alumina for adsorption and defluoridation. This expertise allows M.H.C to serve municipal and industrial water treatment plants with technical support and customized solutions.
Detergent & Cosmetic Raw Materials
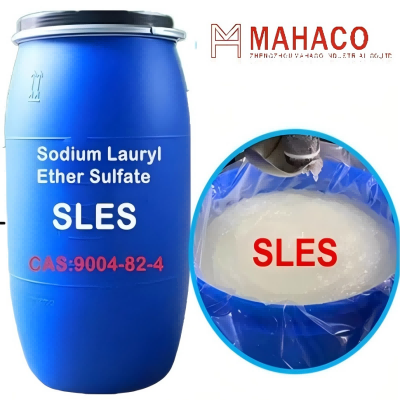
As a key supplier to the household and personal care industries, M.H.C offers a portfolio including Sodium Lauryl Ether Sulfate (SLES), Sodium Tripolyphosphate (STPP), Trisodium Phosphate (TSP), Sodium Metasilicate Pentahydrate, Fatty Alcohol Polyoxyethylene Ether (AEO), and Oxalic Acid. These raw materials are essential for manufacturing detergents, cleaning agents, and cosmetics, and M.H.C ensures consistent quality to meet stringent industry requirements.
Industrial Inorganic Acids, Alkalis & Solvents
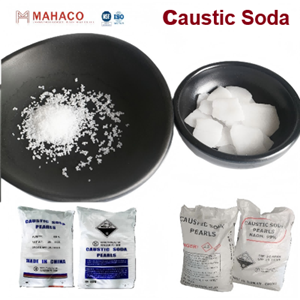
For diverse manufacturing processes, M.H.C supplies essential industrial chemicals such as Nitric Acid (HNO3 68%), Phosphoric Acid 85%, Hydrogen Peroxide, Caustic Soda (Sodium Hydroxide), Potassium Hydroxide (KOH 90% Caustic Potash), Sodium Sulphate Anhydrous, Ammonium Chloride, and various Solvents. These products are critical for pH adjustment, cleaning, and chemical synthesis across industries.
Mining, Food & Specialty Additives
Specialized sectors are also well served. For mining and agriculture, M.H.C offers Zinc Sulphate and Manganese Sulfate. For industrial and food applications, the company supplies Hexamine (Hexamethylenetetramine/Urotropin), Paraformaldehyde (PFA), Aluminium Hydroxide, and Lactic Acid. This diversity highlights M.H.C’s capability to meet niche requirements.
Why Fast Turnaround Times Matter
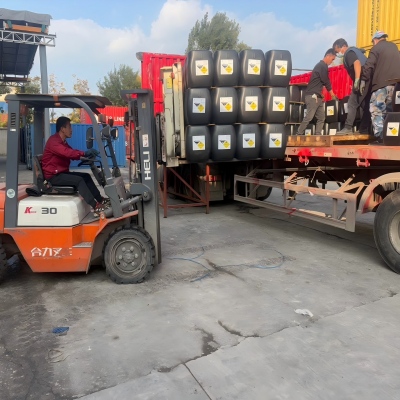
In the chemical industry, delays can halt production and cause significant financial losses. M.H.C’s commitment to fast turnaround times stems from its strategic location in Zhengzhou, a major national transportation hub. With excellent rail, road, and air freight networks, the company can deliver products to major Chinese ports (Qingdao, Tianjin, Shanghai) quickly, reducing lead times and optimizing supply chain management. This logistical advantage translates into competitive freight costs and reliable delivery schedules for international clients.
Quality Control and Sourcing Network
M.H.C maintains long-term partnerships with reputable, ISO-certified manufacturers across China. Every product batch undergoes strict quality inspection before shipment, with certificates of analysis (COA) provided for customer verification. For critical specifications like purity levels – such as Nitric Acid 68%, SHMP 68%, or KOH 90% – M.H.C ensures consistent compliance with international standards. This rigorous approach builds trust and reduces customer risk.
One-Stop Chemical Sourcing Advantage
Clients benefit from M.H.C’s exceptionally broad range of over 50 industrial chemicals from a single supplier. Instead of managing multiple vendor relationships, customers can source water treatment chemicals, detergent raw materials, industrial acids/alkalis, and specialty additives through M.H.C. This one-stop solution significantly reduces procurement complexity, lowers administrative costs, and streamlines logistics coordination. The result is faster turnaround times and enhanced operational efficiency for buyers.
Flexible Packaging and Customized Service
Understanding diverse global requirements, M.H.C offers flexible packaging options including 25kg bags, 50kg drums, IBC totes, and flexitanks based on customer needs. The company provides professional documentation such as MSDS, COA, commercial invoices, and customs clearance support, ensuring smooth international transactions. Whether a client requires a small sample or a full container load, M.H.C delivers promptly.
Proven Track Record and Customer Trust
Over years of operation, M.H.C has built a loyal customer base across Asia, Africa, South America, and Europe. Testimonials and repeat orders from satisfied clients demonstrate the company’s commitment to product quality, on-time delivery, and responsive after-sales service. For example, a water treatment plant in Southeast Asia regularly orders PAC and PolyDADMAC for its coagulation processes, praising M.H.C’s consistency and fast shipping.
Conclusion
Zhengzhou Mahaco Industrial Co., Ltd. stands out as a reliable industrial chemicals manufacturer from China, offering fast turnaround times without compromising on quality. With a comprehensive product portfolio, strategic location, rigorous quality control, and customer-centric service, M.H.C is the ideal partner for global buyers seeking efficient chemical sourcing. To learn more about their products or request a quote, visit their website or contact their sales team.
Summary
Zhengzhou Mahaco Industrial Co., Ltd. (M.H.C) is a professional supplier and manufacturer of high-quality industrial chemicals based in Zhengzhou, China. Known for fast turnaround times, the company offers a comprehensive portfolio including water treatment chemicals (PAC, PFS, PolyDADMAC, etc.), detergent raw materials (SLES, STPP, etc.), industrial acids and alkalis (Nitric Acid 68%, Caustic Soda, etc.), and specialty additives (Zinc Sulphate, Hexamine). Leveraging its strategic location in Central China’s transportation hub, M.H.C ensures rapid delivery to major ports and international clients. The company maintains strict quality control through partnerships with ISO-certified manufacturers and provides certificates of analysis for every batch. Its one-stop sourcing model reduces procurement complexity, while flexible packaging (bags, drums, IBC totes, flexitanks) and professional documentation support facilitate seamless global trade. With a proven track record across Asia, Africa, South America, and Europe, M.H.C is a trusted partner for industries such as water treatment, cosmetics, mining, and food processing, delivering reliability and speed in every shipment.