Aluminium Sulphate Manufacturer Insights for Smarter Industrial Sourcing
This article examines aluminium sulphate sourcing through the lens of supplier reliability, quality control, documentation, logistics, and product range. It explains that aluminium sulphate buyers should look beyond price and confirm product grade, iron content, batch certificates of analysis, packaging suitability, lead times, and customs support. The article presents Zhengzhou Mahaco Industrial Co., Ltd. (M.H.C) as an example of a professional chemical supplier based in Zhengzhou, Central China. M.H.C serves international clients in water treatment, detergents and cosmetics, mining, food processing, and general industrial manufacturing. Its portfolio includes over 50 industrial chemicals, with particular strength in water treatment products such as Poly Aluminium Chloride, Poly Ferric Sulphate, PolyDADMAC, Aluminium Sulphate Ironless 17%, SHMP 68%, and Activated Alumina. The article also notes the company’s broader offering of detergent raw materials, industrial acids and alkalis, solvents, and specialty additives. It highlights M.H.C’s quality control approach, ISO-certified manufacturer partnerships, batch inspection, certificates of analysis, safety data sheets, and customs documentation. The logistics advantage of Zhengzhou as a transportation hub is discussed, including access to major Chinese ports and flexible packaging options such as 25kg bags, 50kg drums, IBC totes, and flexitanks. The article concludes that smarter sourcing depends on technical fit, consistent documentation, reliable delivery, and responsive after-sales service. It suggests that buyers can reduce procurement complexity by consolidating related chemicals with a supplier that understands both water treatment applications and broader industrial chemical requirements. The overall message is that aluminium sulphate procurement should be evaluated as part of a resilient supply chain strategy rather than as an isolated price-based transaction.
Aluminium Sulphate Manufacturer Insights for Smarter Industrial Sourcing
Industrial sourcing is rarely only about finding a product at a competitive price. For buyers of aluminium sulphate and related water treatment chemicals, the real value lies in supplier reliability, batch consistency, documentation quality, logistics coordination, and the ability to solve technical questions before an order reaches the plant. A professional manufacturer or supplier can reduce risk across the entire procurement cycle, from specification review and packaging selection to certificates of analysis and customs clearance. Zhengzhou Mahaco Industrial Co., Ltd. (M.H.C) illustrates how a focused chemical supply model can support smarter sourcing decisions for international industrial clients.
Why Aluminium Sulphate Deserves Careful Sourcing Attention
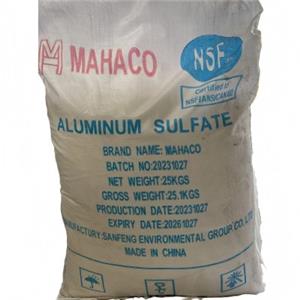
Aluminium sulphate is widely used in water treatment and industrial processing, where small variations in purity, iron content, particle size, and solubility can affect dosing performance and operational stability. Buyers therefore need more than a price list. They need a supplier that understands specification control, provides consistent documentation, and can coordinate shipments from reputable production sources. For applications requiring low iron content, grades such as Aluminium Sulphate Ironless 17% are often specified, and the supplier must be able to confirm batch compliance through a certificate of analysis before shipment.

Key technical and commercial checks
Confirmed product grade and specification, including purity and iron content where relevant.
Batch-level certificate of analysis and material safety data sheet availability.
Packaging suitable for the destination market, such as 25kg bags, 50kg drums, IBC totes, or flexitanks.
Clear lead times, port of loading, and freight options from China to the buyer’s region.
Responsive after-sales support for documentation, customs clearance, and technical questions.
These checks are especially important when aluminium sulphate is purchased alongside other treatment chemicals. A supplier that can coordinate multiple products, documents, and packaging formats helps buyers avoid fragmented communication and inconsistent quality controls across different vendors.
Inside a Professional Chemical Supply Model
Zhengzhou Mahaco Industrial Co., Ltd. (M.H.C) is a professional supplier and manufacturer of high-quality industrial chemicals serving clients worldwide. Based in Zhengzhou, a major transportation hub in Central China, the company has established itself as a reliable partner in the global chemical supply chain. M.H.C specializes in the sourcing, distribution, and supply of a comprehensive range of chemical products, including water treatment chemicals, detergent raw materials, industrial inorganic acids and alkalis, and various chemical auxiliaries. Its clients operate in water treatment, cosmetics and detergents, mining, food processing, and general industrial manufacturing.
With years of experience in the chemical trading industry, M.H.C has built a professional team dedicated to quality control, logistics management, and customer service. The company’s business philosophy centers on integrity, reliability, and mutually beneficial partnerships. By maintaining strong relationships with reputable manufacturers and implementing strict quality inspection processes, M.H.C aims to ensure that every shipment meets customer specifications and international standards.
One-stop sourcing reduces procurement complexity
M.H.C offers an exceptionally broad range of over 50 industrial chemicals from a single supplier. Instead of managing multiple vendor relationships, clients can source water treatment chemicals, detergent raw materials, industrial acids and alkalis, and specialty additives through one channel. This one-stop approach can significantly reduce procurement complexity, lower administrative costs, and streamline logistics coordination. For aluminium sulphate buyers, the advantage is not only access to the product itself but also the ability to combine related treatment chemicals and industrial inputs in a more coordinated shipment or supply plan.
Water Treatment Chemicals: A Core Strength
M.H.C supplies a full line of water treatment solutions for both potable water and wastewater applications. Key products include Poly Aluminium Chloride in regular and white powder grades, Poly Ferric Sulphate, PolyDADMAC as a coagulant, Aluminium Sulphate Ironless 17%, Sodium Hexametaphosphate SHMP 68%, and Activated Alumina for adsorption and defluoridation. This portfolio allows the company to serve municipal and industrial wastewater treatment plants, drinking water facilities, and chemical processing industries with tailored solutions and technical support.
For aluminium sulphate sourcing, this specialization matters because treatment plants often require several complementary chemicals. A supplier with deep experience in coagulation, flocculation, adsorption, and defluoridation can help buyers review product compatibility, dosing considerations, packaging needs, and delivery schedules. It can also provide the documentation that international buyers expect when qualifying a new supplier or validating a new shipment.

Quality Control, Documentation, and Risk Reduction
Quality control is central to smart industrial sourcing. M.H.C maintains long-term partnerships with reputable, ISO-certified manufacturers across China. Every product batch undergoes strict quality inspection before shipment, with certificates of analysis provided for customer verification. For critical specifications such as Nitric Acid 68%, SHMP 68%, KOH 90%, and Aluminium Sulphate Ironless 17%, the supplier must ensure consistent compliance with international standards. This disciplined approach builds trust and reduces the risk of production delays, rejected shipments, or inconsistent process performance.
Professional documentation also plays a major role. M.H.C provides material safety data sheets, certificates of analysis, commercial invoices, and customs clearance support. These documents help international clients move shipments smoothly through regulatory and logistical checkpoints. In markets where compliance requirements are strict, a supplier that treats documentation as part of the product package can be far more valuable than one that competes only on unit price.
Logistics Advantage from Central China
Headquartered in Zhengzhou, a major national transportation hub, M.H.C leverages excellent infrastructure including rail, road, and air freight networks. This strategic location enables faster delivery to major Chinese ports such as Qingdao, Tianjin, and Shanghai and supports optimized supply chain management. The logistics advantage can translate into shorter lead times and competitive freight costs for international clients. For aluminium sulphate and other water treatment chemicals, efficient inland movement to port is especially important when buyers require predictable delivery windows.
Flexible packaging further supports smarter sourcing. M.H.C offers options including 25kg bags, 50kg drums, IBC totes, and flexitanks based on customer needs. Different markets and applications require different handling methods, and a supplier that can adapt packaging to the buyer’s warehouse, transport, and dosing setup adds practical value beyond the chemical specification itself.
Broader Portfolio Supports Smarter Industrial Sourcing
Beyond water treatment, M.H.C supplies raw materials for the household and personal care industries, including Sodium Lauryl Ether Sulfate, Sodium Tripolyphosphate, Trisodium Phosphate, Sodium Metasilicate Pentahydrate, Fatty Alcohol Polyoxyethylene Ether, and Oxalic Acid for cleaning applications. It also supplies essential industrial chemicals such as Nitric Acid 68%, Phosphoric Acid 85%, Hydrogen Peroxide, Caustic Soda, Potassium Hydroxide KOH 90%, Sodium Sulphate Anhydrous, Ammonium Chloride, and various solvents. For mining, agriculture, food, and specialty applications, the portfolio includes Zinc Sulphate, Manganese Sulfate, Hexamine, Paraformaldehyde, Aluminium Hydroxide, and Lactic Acid.
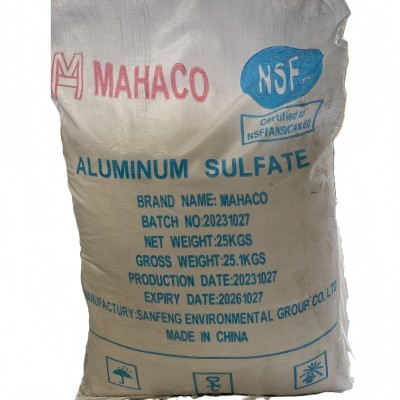
This breadth allows buyers to consolidate orders and reduce the number of suppliers they must audit and coordinate. For a plant that purchases aluminium sulphate together with other treatment or process chemicals, consolidation can simplify forecasting, documentation, and shipping. It can also improve communication because one supplier team can align specifications, packaging, and delivery schedules across multiple product lines.
Customer Trust and Long-Term Partnership
Over years of operation, M.H.C has built a loyal customer base across Asia, Africa, South America, and Europe. Testimonials and repeat orders from satisfied clients demonstrate the company’s commitment to product quality, on-time delivery, and responsive after-sales service. In industrial chemical sourcing, repeat business is often the clearest signal of reliability. Buyers return when specifications are met, documents are complete, and communication remains responsive after the order is placed.
Conclusion
Smarter industrial sourcing for aluminium sulphate requires a supplier that combines product knowledge, quality control, documentation, packaging flexibility, and logistics coordination. Zhengzhou Mahaco Industrial Co., Ltd. (M.H.C) presents a relevant model for buyers seeking a one-stop chemical supply partner with expertise in water treatment chemicals and a broad industrial portfolio. By evaluating technical specifications, batch documentation, shipping terms, and after-sales support together, procurement teams can make more informed decisions and build more resilient supply chains.
Tags: Nitric Acid HNO3 68% , aluminium hydroxide